
Cangzhou Spiral Steel Pipes Group Co.ltd
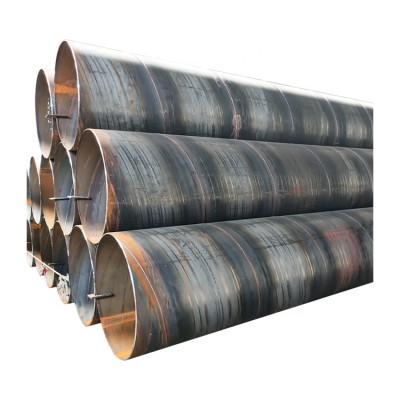
The Solid Foundation for Project SuccessHome / All / Line Pipes / Pipeline for Oil And Gas / API 5L Spiral Welded Line Pipe – SSAW for Oil & Gas Transmission / api 5l x70 pipe
api 5l x70 pipe


| Share | |
|---|---|
| Categories | API 5L Spiral Welded Line Pipe – SSAW for Oil & Gas Transmission |
| Brand | Cangzhou Spiral Steel Pipe Manufacturers |
| Product Specifications | api 5l x70 pipe-01 |
| TRADE TERM | FOB CFR CIF |
| Special Pipe | API Pipe, Other, EMT Pipe, Thick Wall Pipe |
| Section Shape | Round |
| Name | API 5L SSAW Line Pipe |
| Standard | API 5L |
| Technique | SSAW |
| Product name | Spiral Steel Hollow Section |
| Oiled or Non-oiled | Non-oiled |
| Processing Service | Welding, Punching, Cutting, Bending, Decoiling |
| Length | 12M, 6m, 6.4M, 1-30M or custom |
| Certificate | API 5L, CE, JIS, ISO9001,etc |
| Ends | 1.Plain End2. Beveled |
| Material | X70 (L485) |
| Surface Treatment | galvanized,3pe,etc |
| FOB port | Tianjin port |
| Terms of Payment | L/C, T/T |
| Download |  |
Detail Information
API 5L X70 Pipe(Spiral Welded Pipe)
API 5L X70 spiral welded pipe is a high-grade line pipe product with a minimum yield strength requirement of 485 MPa (70,300 PSI) and a minimum tensile strength of 570 MPa (82,700 PSI). It is manufactured to the API 5L specification in two product specification levels, PSL1 and PSL2, with PSL2 imposing stricter limits on carbon, phosphorus and sulfur content as well as tighter requirements for impact toughness and non-destructive testing. Spiral welded pipe is formed and welded from narrower steel strip at a spiral forming angle, so a single strip width can cover a wide diameter range, making it suitable for large-diameter, long-length pipeline projects. Cangzhou Spiral Steel Pipe Manufacturing Group produces API 5L X70 spiral welded pipe on 13 spiral welded pipe lines, with diameter coverage from Φ219 to Φ3620 mm, wall thickness from 6.0 to 25.4 mm, and lengths cut to order up to 30 m, supported by a CNAS-accredited laboratory for chemical composition, tensile, impact, hydrostatic and non-destructive testing.
Delivery Capability
| Item | Range |
| Standard | API 5L (PSL1 or PSL2) |
| Steel grade | X70 (L485) |
| Process | Spiral seam double-sided submerged arc welding (SAWH) |
Diameter | Φ219 – Φ3620 mm |
Wall thickness | 6.0 – 25.4 mm |
Length | 1 – 30 m, cut to order |
Production lines | 13 |
Annual capacity | 400,000 tons |
Testing | CNAS lab: chemical composition, tensile, impact, metallography, hydrostatic, NDT |
Typical use | Oil and gas transmission, high-pressure water, piling, structural |
Surface treatment | Bare, black paint/varnish, anti-rust oil, 3PE/3LPE, FBE, coal tar epoxy, galvanized (on request) |
Pipe end | Plain end, beveled end, threaded end, can be equipped with plastic pipe caps |
heat treatment | PSL2 usually requires normalization or tempering (Q&T, quenching+tempering); X70 PSL2 common TMCP (hot mechanical rolling) delivery status, suffix M; quenching and tempering status suffix Q |
Acidic service | PSL2 only; suffix S (X70MS/X70QS); NACE MR0175/ISO 15156 compliance; HIC and SSC testing required |
Why spiral welded pipe for API 5L X70
Longitudinal welded pipe runs into a diameter ceiling and a cost penalty on large-diameter, high-pressure work. Spiral seam pipe is formed from narrower strip at an angle, so one strip width covers a wide diameter range simply by changing the forming angle. API 5L X70 is a line pipe steel with a minimum yield of 485 MPa. We weld it with double-sided submerged arc welding, inner and outer pass in a single run. The spiral weld runs at an angle to the pipe axis, so hoop stress does not sit parallel to the seam. At the same wall thickness, that gives you more balanced impact and crack resistance, which matters on high-strength transmission pipe in rough ground or under dynamic load.
Large-diameter API 5L X70 spiral welded pipe usually costs less than straight-seam pipe of the same size. Our lines switch across 219–3620 mm and cut to 30 m, so you weld fewer joints on your buried pipeline.
API 5L X70 SSAW Pipe Specification Table
Confirm PSL1 or PSL2 first. PSL2 tightens carbon, phosphorus and sulfur limits and adds impact toughness for sour service or low temperature.
Table 1: Chemical Composition (%, max)
| Element | PSL1 (X70) | PSL2 (X70M/X70Q) |
| C | 0.28 | 0.24 (or 0.12 by agreement) |
| Mn | 1.40 | 1.40 (up to 1.70 by agreement) |
| P | 0.030 | 0.025 |
S | 0.030 | 0.015 |
Si | As required | ≤0.45 |
CEIIW | By agreement | ≤0.43 (typical PSL2) |
The tighter PSL2 limits come from the skelp specification, so the finished chemistry of API 5L X70 spiral steel pipe depends on the plate source your project names. The heat analysis certificate is issued before the contract. | ||
Table 2: Mechanical properties
| Property | PSL1 (X70) | PSL2 (X70M/X70Q) |
| Yield strength Rt0.5 | ≥485 MPa | 485 – 635 MPa |
| Tensile strength Rm | ≥570 MPa | 570 – 760 MPa |
| Yield-to-tensile ratio | As required | ≤0.93 |
Elongation | Per API 5L | Per API 5L, stricter PSL2 |
PSL2 caps yield at 635 MPa to prevent over-strength pipe from softening the field girth weld HAZ. A yield-to-tensile ratio of ≤0.93 confirms the pipe body still has plastic deformation capacity. We take a tensile sample from every batch of API 5L X70 pipe, and the report ships with the order. | ||
Table 3: Charpy impact, pipe body (PSL2, 0°C)
| Diameter | Min. average Kv (J) | Min. single value (J) |
| ≤508 mm | 40 (or as agreed) | 27 |
| >508 – ≤762 mm | 40 | 27 |
| >762 – ≤914 mm | 40 | 27 |
>914 – ≤1219 mm | 40 | 27 |
>1219 – ≤1422 mm | 40 | 27 |
>1422 – ≤2134 mm | 40 | 27 |
For double submerged arc welded pipe, the weld and HAZ require a minimum average of 27 J below 1422 mm and 40 J at 1422 mm and above, at 0°C. The spiral seam is a space curve, so HAZ sample position and test direction must follow API 5L exactly. We prepare SAWH weld impact specimens in-house, and the reports are usable for supervision acceptance. | ||
The three things buyers usually ask us about
The first is whether we can actually hold a delivery date on large-diameter heavy wall. Plenty of traders say they can do Φ3000 and up, then the pipe takes 45 days or more. We run 13 lines with large-diameter and standard-diameter scheduled separately, and 400,000 tons a year gives enough buffer that a thick-wall API 5L X70 order does not get pushed aside by small-diameter work. With diameter coverage to 3620 mm, your design institute does not have to shrink the line because someone said it cannot be made.
The second is weld quality. The spiral seam is a space curve, so it is harder to inspect than a straight seam. We sample every batch for ultrasonic or X-ray on the weld, and hydro test pipe by pipe to API 5L. What you get is not a photocopied certificate. It is a traceable package with the plate heat number, the welding parameters, and the tensile and impact report numbers. On PSL2 orders the carbon equivalent and the impact data above are run and filed to standard.
The third is length. Most spiral pipe ships at 12–18 m. We cut 1–30 m. On a river crossing or a remote spread, going to 24 m or 30 m takes more than a third of the field girth welds out of the job, and lifting and fit-up get easier. One caveat on 30 m: check the transport route for oversize permits before you commit, and we will go through the transport plan with you before the contract.
Next Step
You do not need to go through a trading layer. Send our technical sales three things: diameter and wall thickness, PSL grade, and delivery length plus destination. You get a factory quotation with a firm delivery date and the inspection standard inside 24 hours. If you have a project spec or a coating requirement (3PE, FBE, epoxy), attach it and we will line up the coating schedule at the same time.
Cangzhou Spiral Steel Pipe Manufacturing Group | 13 lines · CNAS lab · 400,000 t/year · Φ219–3620 mm · wall 6–25.4 mm · cut 1–30 m

Related Products


Review
- 加载中···
We provide you with free spiral steel pipe manufacturing consulting services. Whether you have any questions about project design, material selection or technical parameters, our team of experts will provide you with professional advice.
Contact us now to get free technical consultation and personalized solutions and quotes
- Phone
- *Title
- *Content