
Cangzhou Spiral Steel Pipes Group Co.ltd
The Solid Foundation for Project SuccessHome / All / Line Pipes / Pipeline for Oil And Gas / API 5L Spiral Welded Line Pipe – SSAW for Oil & Gas Transmission / api 5l x52 psl2 pipe
api 5l x52 psl2 pipe


| Share | |
|---|---|
| Categories | API 5L Spiral Welded Line Pipe – SSAW for Oil & Gas Transmission |
| Brand | Cangzhou Spiral Steel Pipe Manufacturers |
| Model | api 5l x52 pipe-01 |
| TRADE TERM | FOB CFR CIF EXW |
| Special Pipe | API Pipe, Other, EMT Pipe, Thick Wall Pipe |
| Name | API 5L SSAW Line Pipe |
| Standard | API 5L ISO3183 |
| Technique | SSAW(Spiral welded) |
| Certificate | API 5L, CE, JIS, ISO9001,ISO14001,ISO45001,BV,etc. |
| Product name | API 5L X52 Pipe |
| Wall Thickness Schedule | SCH 40, SCH STD, SCH80, SCH XS, SCH 160, etc |
| Processing Service | Welding, Punching, Cutting, Bending, Decoiling |
| Length | 12M, 6m, 6.4M,18M-30M(DRL SRL 20FT 40FT) or Custom |
| Surface | Black Painting, Varnished, FBE, 3PE, 3LPE, 3PP, CRA clad and lined pipe |
| Ends | 1.Plain End2. Beveled3.Threaded.4 Screwed |
| Material | X52 or L390 (N, Q, M, R) in PSL1 and PSL2 |
| Outer Diameter | 8.62"-142"(219-3620mm) |
| FOB port | Tianjin port |
| Terms of Payment | L/C, T/T |
| Download |  |
Detail Information
Asia’s First 30m SSAW Pipe Producer | CNAS-Certified Lab | 13 Integrated Production Lines — One-Stop Quality Assurance
API 5L X52 pipe, also called L360 pipe, is named after its minimum yield strength of 52 Ksi (360 MPa). It is a medium-grade specification within the API 5L and ISO 3183 standards, widely used for oil and gas pipeline transmissions. As one of the flagship products of Cangzhou Spiral Steel Pipe Manufacturing Group Co., Ltd., our X52 SSAW pipes are manufactured using double-sided submerged-arc spiral welding technology. Backed by our CNAS-accredited laboratory and 13 integrated production lines covering everything from steel coil forming to anti-corrosion coating, we are the first manufacturer in Asia capable of producing spiral welded pipes up to 30 meters in length. This fully integrated in-house process eliminates the quality risks typically associated with fragmented multi-factory processing, ensuring you receive consistent, reliable pipe performance for your critical pipeline projects.
Delivery Condition And API 5L X52 Pipe Types
Scope divided by product specification level: PSL1, PSL2, sour service:
| API 5L X52 PSL1 | for the pipes in common delivery condition of As Rolled |
| API 5L X52N/M/Q | for PSL2 pipe with delivery condition of N, M, and Q. |
| API 5L X52NS/MS/QS | for PSL2 pipes with sour services. |
Suffix Letter Means R: As rolled N: Normalizing rolled, Normalized formed, Normalized Q: Tempered and quenched M: Thermomechanical rolled or thermomechanical formed S: Sour Service | |
When the finished product of Wuzhou Brand API 5L X52 spiral steel pipe is delivered, the manufacturing process adopts the spiral double-sided submerged arc welding process.
Our Manufacturing Edge: With 13 parallel production lines covering the entire process from uncoiling to FBE/3PE coating, and Asia's first 30-meter SSAW pipe production capability, we offer you reduced on-site welding joints and minimized logistics costs. Our CNAS-certified testing laboratory ensures every pipe meets stringent API 5L PSL2 requirements, giving you full confidence in product quality.
API 5L Grade X52 Pipe Specification
API 5L Pipe Data Sheet, other grades specifications in API 5L.
API 5L X52 Pipe Data Sheet, including PSL1, PSL2, and Sour Services.
API 5L X52 PSL1 Chemical and Mechanical Properties
| Chemical Composition API 5L X52 PSL1 | ||||||||
Steel Grade(Steel Name) | Mass fraction,based upon heat and product analysesa,g | |||||||
| % | ||||||||
C | Mn | P | S | V | Nb | Ti | ||
MAXb | MAXb | MIN | MAX | MAX | MAX | MAX | MAX | |
Welded Steel Pipe | ||||||||
| X52 Or L360 | 0.26 | 1.4 | - | 0.03 | 0.03 | d | d | d |
| a. Cu≤0.50%; Ni≤0.50% and Mo≤0.15 % b. For each reduction of 0.01% below the specified maximum concentration for carbon, an increase of 0.05 % above the specified maximum concentration for Mn is permissible, up tp a maximum of 1.65 % for grade≥ L245 or B, but ≤ L360 or X52; up to a maximum of 1.75% for grade > L360 or X52, but < L485 or X70; and up to a maximum of 2.00% for grade L485 or X70. c. Unless otherwise agreed, Nb + V0,06 %. d.Nb+V+Ti0,15%. e. Unless otherwise agreed. f. Unless otherwise agreed, Nb + V +Ti ≤ 0.001% g. No deliberate addition of B is permitted and the residual B ≤ 0.001 %. | ||||||||
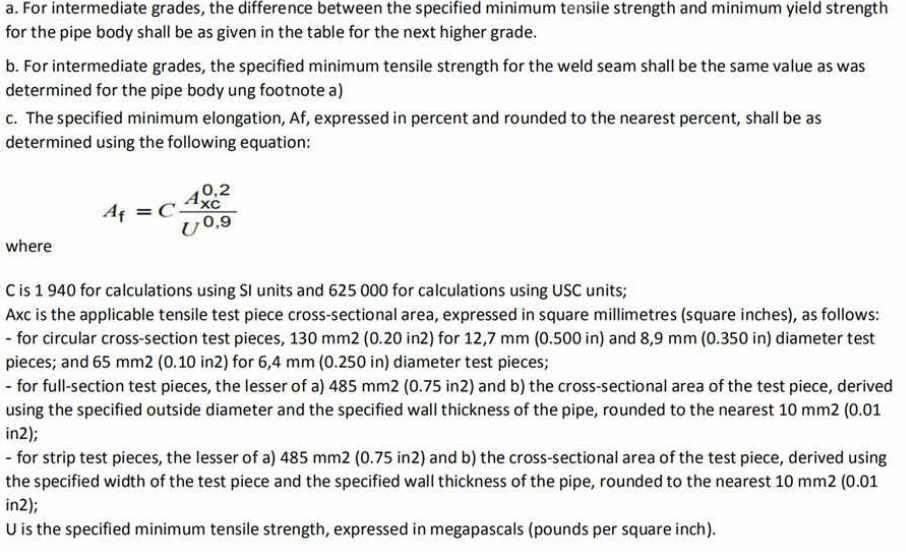
Mechanical Properties for API 5L X52 PSL1 Pipe | ||||
Pipe Grade | Pipe body of welded pipes | Weld seam of EW, LW | ||
| Yield strength a | Tensile strength a | Elongation | Tensile strength b | |
| Rt0.5 | Rm | Af | Rm | |
| MPa (psi) | MPa (psi) | % | MPa (psi) | |
| minimum | minimum | minimum | minimum | |
X52 Or L360 | 360 (52 200) | 570 (82700) | c | 460 (66 700) |
API 5L X52 PSL2 Pipe Data Sheet
X52, L360 PSL2 Chemical Composition
ChemicalComposition API5L X52 PSL2 | |||||||||||
Steel Grade | Mass fraction,based upon heat and product analyses | Carbon equivalent % maximum | |||||||||
% | |||||||||||
Cb | Si | Mnb | P | S | V | Nb | Ti | Other | CEIIw | CEPcm | |
| X52N/L360N | 0.24 | 0.45 | 1.40 | 0.025 | 0.015 | 0.10 | 0.05 | 0.04 | d,e,l | 0.43 | 0.25 |
| X52Q/L360Q | 0.18 | 0.45 | 1.50 | 0.025 | 0.015 | 0.05 | 0.05 | 0.04 | e,l | 0.43 | 0.25 |
| X52M/L360M | 0.22 | 0.45 | 1.40 | 0.025 | 0.015 | d | d | d | e,l | 0.43 | 0.25 |
a. Based upon product analysis. For seamless pipe wth t> 20.0mm (0.787in), the CE limits shal be agreed. The CEIIW limits apply if C>0.12 % and the CEpcm limits apply if C ≤0.12%.
b.For each reduction of 0.01% below the specified maximum concentration for carbon, an increase of 0.05 % above the specified maximum for Mn is permissible, up tp a maximum of 1.65 % for grade ≥L245 or B, buts L360 orX52; up to a maximum of 1.75% for grade > L360 or X52, but <L485 or X70;and up toa maximum of 2.00% for grade L485 or X70, but ≤ L555 or x80, and up to a maximum of 2.20 % for grades> L555 or x80
c. Unless otherwise agreed, Nb + V0,06 %.
d.Nb+V+Ti0,15%.
e. Unless otherwise agreed, Cu 0,50%; Ni 0,30 %; Cr 0,30% and Mo 0,15 %
f. Unless otherwise agreed.
g. Unlessotherwise agreed, Nb + V + Tis0.15 %.
h. Unless otherwise agreed, Cu ≤0.50%; Ni≤ 0.50%; Cr ≤0.50 % and Mo ≤0.15 %
i. Unless otherwise agreed, Cu≤0.50%; Ni≤ 1.00%; Cr≤0.50% and Mo≤0.50%
j.B 0,004 %
k. Unless otherwise agreed, Cu 0,50%; Ni1,00%; Cr 0,55% and Mo 0,80%.
L For all PSL2 pipe grades except those grades to which footnote j already applies, the fllowing applies. Unless otherwise agreed no intentional addition of B is permitted and residual B 0.001%.
X52, L360 PSL2 Pipe Mechnical Properties
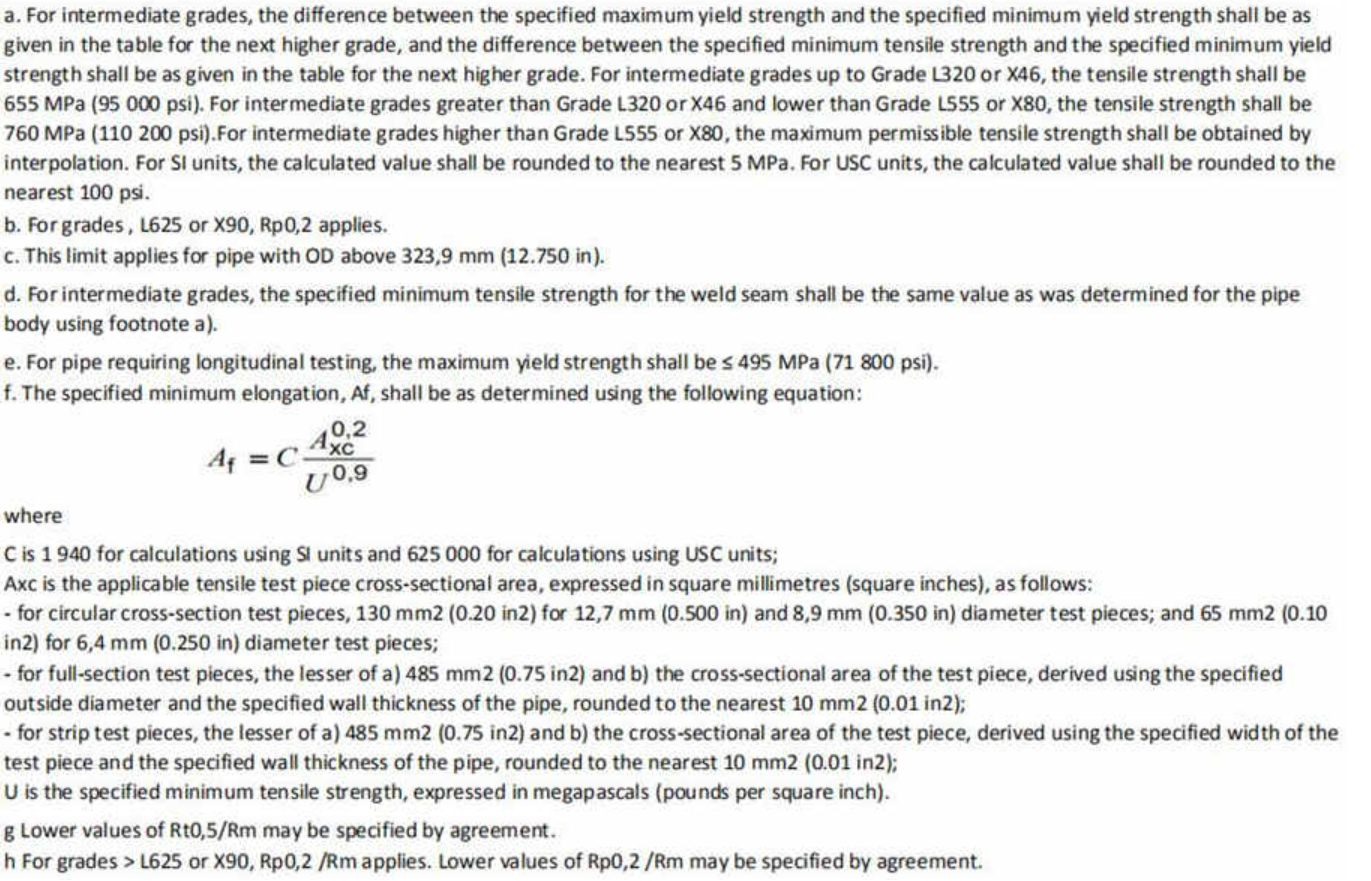
Mechanical Properties for API5L X52 PSL2 pipe | |||||||
Pipe Grade | Pipe body of seamiess and welded pipes | Weld seam of EW, LW, | |||||
Yield strength a | Tensile strength b | Ratio a,c | Elongation (on 50 mm or 2 | Tensile strength d | |||
Rt0.5 | Rm | Rt0.5/Rm | Af | Rm | |||
MPa (psi) | MPa (psi) | % | MPa (psi) | ||||
minimum | maximum | minimum | maximum | maximum | minimum | minimum | |
L360N or X52N L360QorX52Q L360Mor X52M | 360(52200) | 530(76900) | 460(66700) | 760(110200) | 0.93 | f | 460(66700) |
X52 PSL2 vs PSL1 Comparision
API 5L Grade X52 Pipe
Chemical Composition and Mechanical Properties
| Chemical Composition | ||||
| Steel grade (Steel name) | Mass fraction, based upon heat andproduct analyses | |||
% | ||||
C | Mn | P | S | |
max | max | max | max | |
PSL 1 pipe with t ≤ 25.0 mm (0.984 in) | ||||
Welded pipe | ||||
X52 | 0.26 | 1.40 | 0.030 | 0.030 |
PSL 2 pipe with t ≤ 25.0 mm (0.984 in) | ||||
Welded pipe | ||||
X52M | 0.22 | 1.40 | 0.025 | 0.015 |
| Mechanical Properties | |||||
| Pipe Grade | Pipe body of seamless and welded pipes | Weld seam of EW, LW, SAW and COW pipes | |||
| Yield strength | Tensile strength | Tensile strength | |||
| MPa (psi) | MPa (psi) | MPa (psi), min | |||
PSL 1 pipe | 460 (66 700) | ||||
X52 | minimum | minimum | |||
360 (52 200) | 460 (66 700) | ||||
PSL 2 pipe | |||||
X52N X52Q | minimum | maximum | minimum | maximum | |
360 (52 200) | 530 (76 900) | 460 (66 700) | 760 (110 200) | ||
The maximum chemical content of API 5L X52 (L360) PSL2 spiral welded steel pipe is different from that of PSL1; And mechanical strength, more stringent.
API 5L X52 Pipe Pressure Rating (Mechanical Strength)
When you choose X52 (also known as L360) from API 5L, you will find that its minimum yield strength is 52220 psi (360 MPa) and tensile strength is 66700 psi (460 MPa) - it is these two values that determine why it is called X52 or L360. Compared to X46, X42, and Grade B, X52 has superior performance, making it the most common material selection requirement in oil and gas pipeline systems, second only to the highest grade.
For X52 pipes, you need to note that whether you choose seamless pipes or welded pipes (including SSAW ERW LSAW), their pressure rating, tensile strength, and yield strength are the same and do not vary depending on the manufacturing process.
When your operating conditions require higher pressure, you need to increase the wall thickness of the steel pipe accordingly, or switch to a higher grade material in the API 5L standard.
Test Requirements:
Hydrostatic Pressure Test
When conducting a hydrostatic pressure test, you must perform a 100% hydrostatic pressure test on the steel pipes to ensure there are no leaks in the welds or the pipe body. If the pipe sections being used have already successfully passed the hydrostatic pressure test, you do not need to repeat this test on the connections or joints between the sections.
Bending Test
When conducting a bending test, pay close attention—no cracks should appear anywhere on the test specimen, nor should any cracking occur at the welds.
Flattening Test
The flattening test is used to evaluate the performance of steel pipes under compressive deformation. You must use this test to assess the pipe’s resistance to longitudinal and circumferential cracking, including the detection of internal and external defects.
This test must be performed on ERW welded steel pipes with a diameter greater than 12.75 inches;
for steel pipes with an outer diameter-to-wall thickness ratio (OD/WT) greater than 10, no cracking shall occur in the weld until the distance between the two compression plates is less than 30% of the original outer diameter.
Guided Bend Test
In the guided bend test, you must check whether the test specimen has completely fractured, while also noting any cracks or fractures in the weld metal exceeding 3.2 mm in length—regardless of their depth. Additionally, you must deem the test specimen non-conforming if cracks exceeding 3.2 mm in length or 12.5% of the wall thickness in depth are found in the base metal, heat-affected zone (HAZ), or fusion line.
Charpy V-Notch Impact Test (CVN)
This test is mandatory for PSL2-grade pipes. You must take samples based on the pipe type: for seamless pipes, only the pipe body needs to be tested; for welded pipes, impact tests must be performed separately on the pipe body, the weld, and the heat-affected zone (HAZ).
Drop Weight Tear Test (DWTT)
For PSL2-rated pipes, you must also perform the Drop Weight Tear Test (DWTT), which is another mandatory requirement.
If you need to order X52 pipe, here is an example of the specifications:
Item: 4,800 meters of carbon steel pipe, material grade API 5L X52 PSL2 (equivalent to ISO 3183 L-360N), outer diameter 20 inches, manufactured using the spiral submerged arc welding (SSAW) process, with a wall thickness of 0.562 inches. The outer surface of the pipe must be coated with a fusion-bonded epoxy (FBE) powder coating or an equivalent adhesive epoxy external coating.
Why partner with us?
Why partner with us? Our integrated manufacturing base in Cangzhou eliminates the need for you to coordinate between separate factories for forming, welding, and coating — all processes are completed in-house across our 13 production lines. As Asia's pioneer in 30-meter SSAW pipe production, we help you reduce field weld counts by up to 50%. Combined with our CNAS-accredited laboratory's rigorous testing regime, we deliver pipes that perform reliably in the most demanding oil and gas environments.

Related Products


Review
- 加载中···
We provide you with free spiral steel pipe manufacturing consulting services. Whether you have any questions about project design, material selection or technical parameters, our team of experts will provide you with professional advice.
Contact us now to get free technical consultation and personalized solutions and quotes
- Phone
- *Title
- *Content