
Cangzhou Spiral Steel Pipes Group Co.ltd
The Solid Foundation for Project SuccessAwwa C200 Spiral Welded Steel Pipe
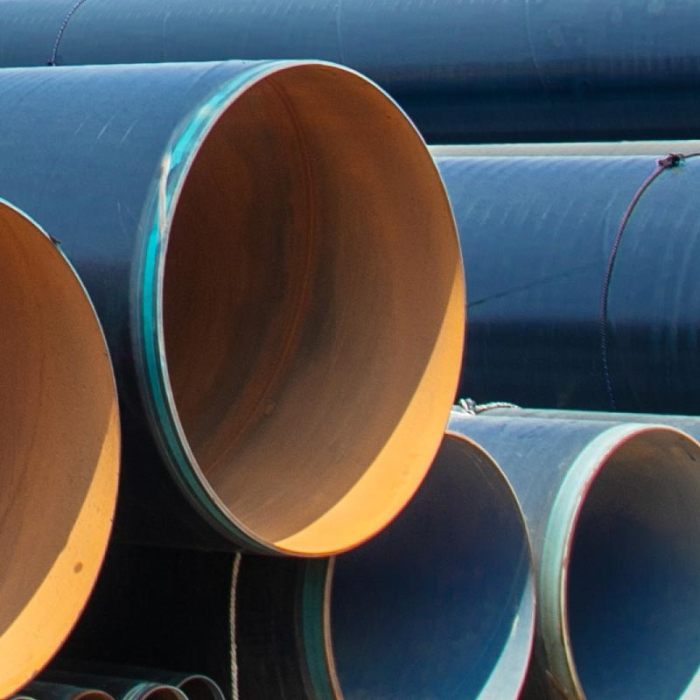

Detail Information
AWWA C200 Spiral Welded Steel Pipe for Water Transmission
Cangzhou Spiral Welded Pipe Manufacturing Group — 13 Production Lines, 400,000 Tons Annual Capacity, CNAS Certified Laboratory
13 Production Lines | 400,000 Tons/Year | 8 inch to 120 inch OD | CNAS Certified Lab
What Is AWWA C200 and Why Spiral Welded Pipe Is the Preferred Choice for Water Transmission
AWWA C200 is the American Water Works Association standard for steel water pipe, 6 inches (150 mm) and larger, used for the transmission and distribution of potable water, raw water, reclaimed water, and wastewater. This standard covers electrically butt-welded straight-seam or spiral-seam steel pipe, establishing requirements for fabrication, welding operations, permissible variations, end preparation, inspection, and testing procedures.
Spiral welded steel pipe, also known as SSAW pipe, is manufactured by spirally coiling steel strip and welding the seam with a double submerged arc process. The spiral seam distributes circumferential stress more evenly than a straight longitudinal seam, which improves the pipe's structural performance under internal pressure and external soil loads. The continuous coil-fed production method also delivers higher dimensional consistency across long production runs, making spiral welded pipe particularly well-suited for large-diameter water mains, transmission mains, and aqueducts where uniform wall thickness and accurate diameter are critical to installation efficiency and long-term service life.
Product Specifications
| Parameter | Range |
| Outside Diameter | 219 mm to 3048 mm (8 inch to 120 inch) |
| Wall Thickness | 6.0 mm to 25.4 mm |
| Length | 6 m to 50 m (custom lengths available) |
Steel Grades | ASTM A139 Gr.B, API 5L B/X42/X52, ASTM A36 |
Reference Standards | AWWA C200, ASTM A139, API 5L, EN 10219 |
Pipe Ends | Plain end, beveled end, bell and spigot, flanged |
Joint Types | Butt-welded, rubber gasket push-on, mechanical coupling K10/K20 |
The 13 production lines at Cangzhou Spiral Welded Pipe Manufacturing Group cover the full diameter range specified above. With an annual capacity of 400,000 tons, the mill can schedule large-diameter orders in parallel across multiple lines, reducing delivery lead time compared to single-line operations.
Lining and Coating Systems
The lining and coating system has a greater impact on long-term pipeline performance than the steel grade itself. Bare steel is rarely specified for buried water transmission service, and the choice of lining and coating determines resistance to corrosion, tuberculation, and mechanical damage during installation.
Internal Lining Options for Water Service
| Lining Type | Reference Standard | Typical Thickness | Best Application |
| Cement Mortar | AWWA C205 | 6 mm to 13 mm, by pipe diameter | Potable water, raw water, wastewater; passivates steel surface and prevents tuberculation |
| Fusion Bonded Epoxy | AWWA C213 | 0.3 to 0.5 mm | High-temperature service, smaller diameter pipe |
| Polyurethane | AWWA C222 | 0.5 to 1.5 mm | Aggressive water chemistry, high chloride or high TDS |
Liquid Epoxy | AWWA C210 | 0.3 to 0.6 mm | Pump station piping, smaller diameter service lines |
Cement mortar lining raises the effective pH at the steel surface to approximately 12, which passivates the steel and prevents tuberculation. AWWA C205 sets minimum lining thickness by pipe diameter as follows:
| Pipe Diameter (inch) | Pipe Diameter (mm) | Nominal Lining Thickness |
| 4 to 10 | 100 to 250 | 1/4 in (6 mm) |
| 11 to 23 | 275 to 575 | 5/16 in (8 mm) |
| 24 to 36 | 600 to 900 | 3/8 in (10 mm) |
Over 36 | Over 900 | 1/2 in (13 mm) |
A specification that states only "cement mortar lining" without specifying thickness by diameter leaves room for a 6 mm lining to be applied to a 96-inch pipe, which significantly shortens service life. Always include the AWWA C205 thickness table in the procurement specification. Refer to the AWWA C205 table for lining thickness by pipe diameter.
Polyurethane lining is specified where water chemistry is aggressive, including high chloride, high total dissolved solids, or desalinated water service. Polyurethane is smoother than cement mortar, with a Hazen-Williams C factor of approximately 140 to 150, which reduces pumping energy. However, polyurethane lining is less tolerant of installation damage than cement mortar and requires more careful handling on site.
External Coating Options for Buried Service
| Coating Type | Reference Standard | Typical Thickness |
| 3LPE (Three-Layer Polyethylene) | DIN 30670, EN ISO 21809-1 | 2.0 to 3.7 mm, depending on pipe diameter and coating class |
| Fusion Bonded Epoxy | AWWA C213, EN ISO 21809-2 | 0.3 to 0.5 mm |
| Polyethylene Tape Wrap | AWWA C214, EN 12068 | 1.5 to 3.0 mm |
3LPE is the default external coating for buried water transmission mains. The system consists of an FBE primer, a copolymer adhesive layer, and a polyethylene top coat. Total coating thickness varies with pipe diameter and coating class: for pipe diameters from 159 mm to 273 mm in normal class, total thickness is typically 2.0 mm; for pipe diameters from 813 mm to 1420 mm in normal class, total thickness is typically 3.0 mm; for pipe diameters from 813 mm to 1420 mm in special class, total thickness can reach 3.7 mm. Under EN ISO 21809-1, total thickness may extend up to approximately 4.7 mm depending on the class and PE layer minimum thickness.
Coating Adhesion and Surface Preparation
The single most common cause of coating failure in buried service is inadequate anchor pattern depth before coating application. Shot blasting at excessive speed can produce a surface that appears to meet Sa 2.5 cleanliness standards while the anchor pattern depth falls below the required range. This causes the coating to peel from the steel surface over large areas during transportation or under underground soil stress, creating conditions for crevice corrosion.
At Cangzhou Spiral Welded Pipe Manufacturing Group, anchor pattern depth is measured and recorded for every production batch in accordance with the applicable coating standard and our approved coating procedure. Coating adhesion is tested using the pull-off method in our CNAS certified laboratory. The test data is submitted with the mill test certificate for each order.
Manufacturing Process: From Steel Coil to Certified Pipe
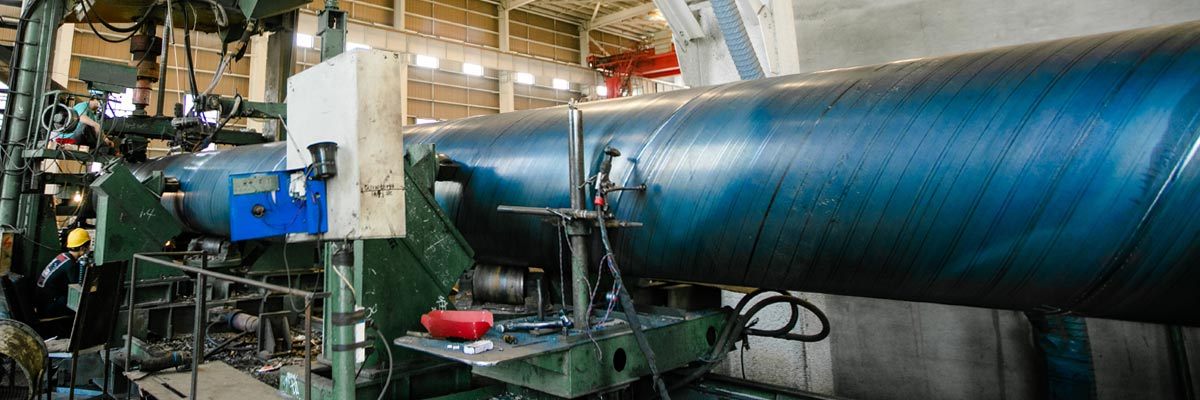
The SSAW manufacturing process follows a defined sequence:
Coil Preparation: Steel strip is uncoiled, leveled, and edge-milled to the required width for the target pipe diameter. Strip edges are cleaned to remove rust and contaminants that could cause porosity or lack of fusion during welding.
Spiral Forming: The strip is fed into a forming machine at a controlled angle, creating the spiral seam geometry. The forming machine controls the spiral angle and strip alignment to prevent misalignment, which weakens the weld's pressure-bearing capacity.
Welding: The spiral seam is welded using the double submerged arc welding process. An initial penetrating weld is made on the inside seam, followed by a second weld along the outside seam. This two-pass weld creates a pipe structure in which the weld is as strong as or stronger than the parent metal.
Weld Inspection: Every length of pipe receives 100 percent ultrasonic testing of the weld seam. In-line continuous UT is supplemented by off-line X-ray radiography. End welds at both pipe ends receive additional 100 percent manual ultrasonic re-inspection because stress conditions during forming are less stable at the ends than in the middle of the pipe.
Hydrostatic Testing: Every pipe receives a hydrostatic test before coating application. The test pressure is specified by the project; if no pressure is specified, the mill applies a standard test pressure and records the pressure-time graph with the mill test certificate.
End Preparation: Pipe ends are machined to the specified configuration. Butt-welded joint ends receive machine-beveled ends per ASME B16.25. Rubber gasket joint ends receive bell and spigot forming with K10 or K20 steel rings for mechanical coupling systems.
Coating Application: Lining and coating are applied in the same facility under the same quality management system. Cement mortar lining is applied by centrifugal or spray method. 3LPE external coating is applied by side extrusion or powder spray. FBE is applied by electrostatic spray.
Quality Assurance and Third-Party Inspection
The quality assurance program at Cangzhou Spiral Welded Pipe Manufacturing Group is designed to support the requirements of third-party inspection agencies including SGS, BV, and TUV.
Certified Welding Inspectors: The mill employs Certified Welding Inspectors (CWI) qualified under AWS QC1. CWIs perform 100 percent visual examination of every weld as a minimum requirement.
Laboratory Testing: The CNAS certified laboratory performs chemical analysis, tensile testing, Charpy V-notch impact testing, and coating adhesion testing on every production heat. Test reports are traceable to the heat number and pipe mark number.
Mill Test Certificates: Each shipment is accompanied by EN 10204 3.1 mill test certificates containing chemical composition, tensile properties, elongation, and hydrostatic test results. Charpy impact test results are included when specified. Pressure-time graphs for hydrostatic testing are retained and available upon request.
Dimensional Verification: OD tolerance, ovality, straightness, end squareness, and bevel angle are measured for every pipe. Shop fit tests are performed to verify that joints assemble correctly and that annular space between spigot and bell meets AWWA C200 requirements.
Third-Party Access: Buyers or their designated inspection agencies may access the production areas relevant to their order. Advance notice allows scheduling of witnessed hydrostatic testing and coating inspection.
Traceability: The mill maintains heat number traceability from steel coil through finished pipe. Welding procedure specifications, procedure qualification records, and welder qualification records are maintained for every welding process and every welder.
Why Cangzhou Spiral Welded Pipe Manufacturing Group
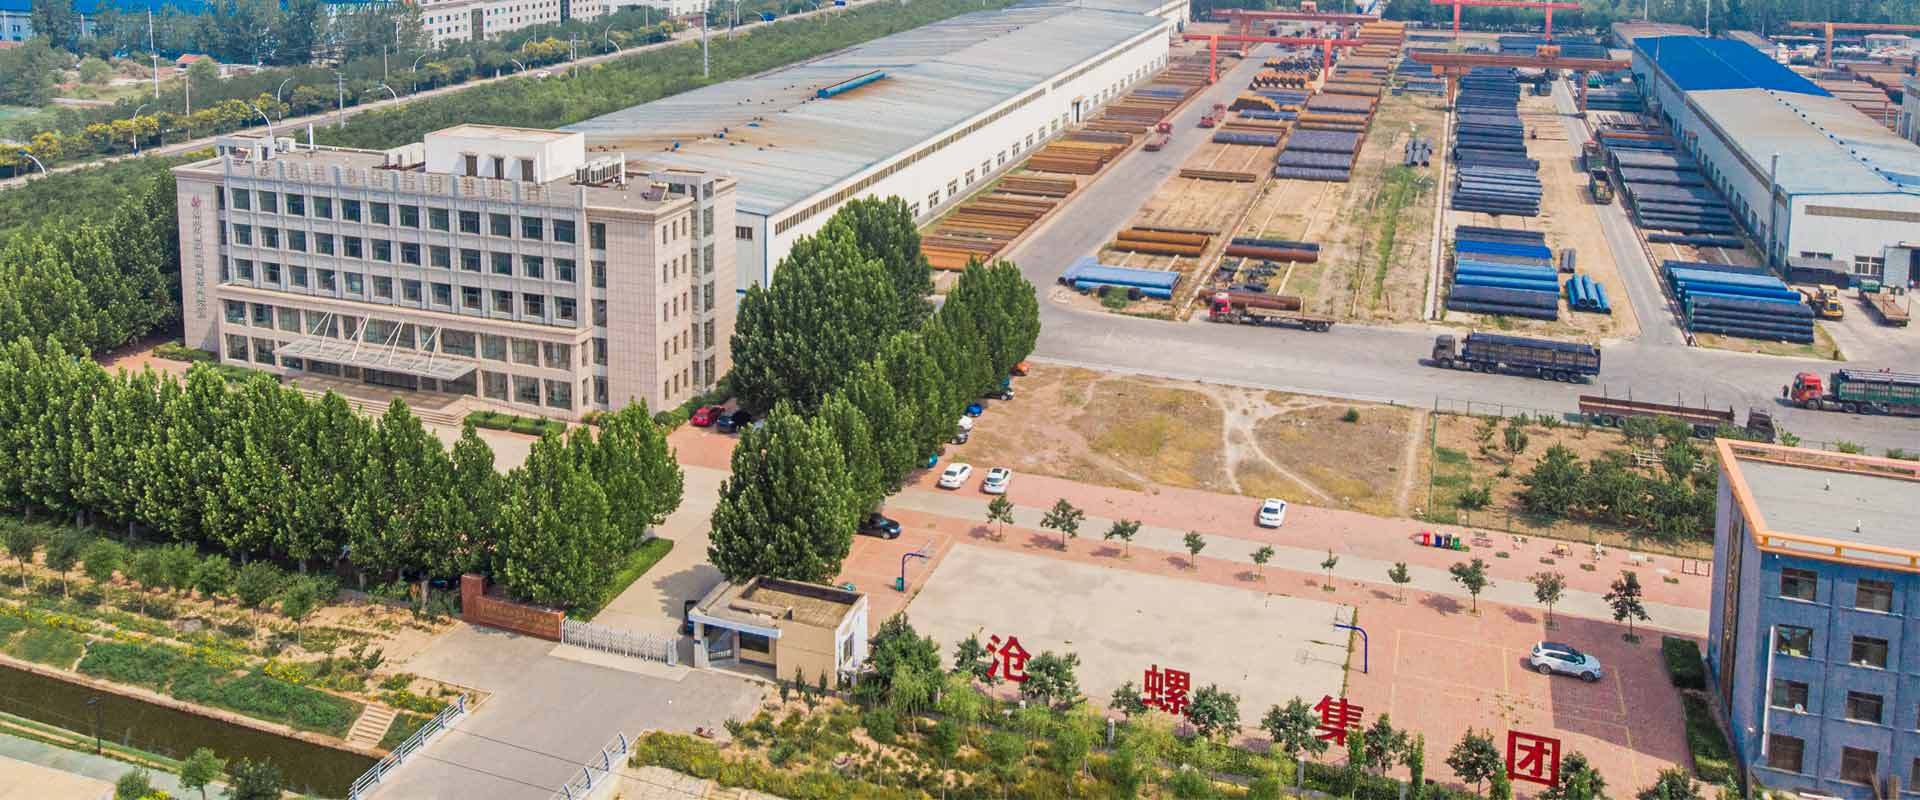
Integrated Manufacturing: Pipe rolling and coating operations are performed at the same facility under one quality management system. This eliminates the responsibility gap that occurs when pipe and coating are produced by separate companies, and it ensures that coating application parameters are controlled as part of the same production record as the pipe itself.
Production Scale: 13 spiral welded pipe production lines with a combined annual capacity of 400,000 tons. This capacity allows parallel scheduling of large-diameter orders, reducing delivery lead time compared to single-line mills.
CNAS Certified Laboratory: Chemical, mechanical, and coating adhesion testing are performed in-house. Pre-shipment test data is available without waiting for third-party laboratory scheduling, which shortens the inspection and release cycle.
Experience with International Water Projects: The mill has supplied AWWA C200 spiral welded pipe to water transmission projects in Southeast Asia, the Middle East, and South America. Project references are available upon request.
Full Traceability Documentation: Every pipe is traceable to its steel heat number. Mill test certificates, welding procedure records, welder qualification records, and coating test reports are compiled for each order.
Frequently Asked Questions
Q1: Do you provide mill test certificates per EN 10204 3.1?
Yes. Every shipment is accompanied by EN 10204 3.1 mill test certificates containing chemical composition, tensile properties, elongation, and hydrostatic test results. Charpy impact test results are included when specified.
Q2: Can I get a sample section of pipe before placing a full order?
Yes. Short sections of pipe can be provided for evaluation. Coating and lining must match the project specification for the sample to be representative. Sample and freight costs are the responsibility of the buyer.
Q3: How do you control weld quality on the spiral seam?
Every weld receives 100 percent ultrasonic testing. In-line continuous UT is supplemented by off-line X-ray radiography. End welds receive additional 100 percent manual ultrasonic re-inspection because forming stresses are less stable at the pipe ends.
Q4: What is the difference between AWWA C200 and ASTM A139 pipe?
AWWA C200 is specifically written for water transmission and distribution systems, with requirements for hydrostatic testing, sanitary compliance, and fabrication of specials. ASTM A139 is a general specification for electric-fusion welded steel pipe. Water projects should specify AWWA C200 as the governing standard.
Q5: Which lining should I specify for potable water versus raw water?
For potable water, specify cement mortar lining per AWWA C205 with thickness by diameter, or FBE lining per AWWA C213. The coating system must be certified to NSF/ANSI 61 or an equivalent water safety approval. For raw water and cooling water, cement mortar lining is acceptable. For aggressive water chemistry with high chloride or high TDS, specify polyurethane lining per AWWA C222.
Q6: What is the correct cement mortar lining thickness for a 48-inch pipe?
Under AWWA C205, a 48-inch pipe falls in the 24 to 36 inch diameter range only if the nominal diameter is 36 inches or less. A 48-inch pipe is over 36 inches, so the minimum cement mortar lining thickness is 1/2 inch (13 mm). For a 24-inch pipe, the minimum is 3/8 inch (10 mm). For an 11 to 23 inch pipe, the minimum is 5/16 inch (8 mm). Always include the AWWA C205 thickness table in the specification rather than stating only "cement mortar lining."
Q7: What is your delivery lead time for 5,000 tons of 48-inch AWWA C200 pipe?
Lead time depends on coating type and current production schedule. Bare pipe typically ships in 30 to 45 days. Cement mortar lined pipe with 3LPE external coating typically ships in 45 to 60 days. The 13 production lines provide scheduling flexibility for large orders.
Q8: Do you allow third-party inspection during production?
Yes. Buyers or their designated inspection agencies may access production areas relevant to their order with advance notice. We provide facilities and testing cooperation for witnessed hydrostatic testing and coating inspection.
Q9: How do you ensure coating adhesion meets specification?
Anchor pattern depth is measured and recorded for each production batch in accordance with the applicable coating standard and our approved coating procedure. Coating adhesion is tested using the pull-off method in our CNAS certified laboratory. Test data is submitted with the mill test certificate.
Q10: What pipe end configurations do you offer?
We offer plain end, beveled end for field butt welding, bell and spigot with rubber gasket for push-on joints, and flanged ends. Bell and spigot pipe can be supplied with K10 or K20 steel rings for mechanical coupling systems.
Request a Quotation or Mill Test Certificate Sample
To receive a quotation or a sample mill test certificate for AWWA C200 spiral welded steel pipe, provide the following information:
Pipe outside diameter and wall thickness
Total quantity in meters or tons
Lining type and thickness
External coating type
Pipe end configuration
Destination port
Quotations are provided within 24 hours of receiving complete specifications.
Review
- 加载中···
We provide you with free spiral steel pipe manufacturing consulting services. Whether you have any questions about project design, material selection or technical parameters, our team of experts will provide you with professional advice.
Contact us now to get free technical consultation and personalized solutions and quotes
- Phone
- *Title
- *Content